Rubber Cutting Blades: Straight, Circular, and Serrated Options Explained

Straight blades give you the cleanest cut on flat rubber sheet, circular blades handle continuous roll-to-roll slitting at speed, and serrated blades are what you reach for when the rubber is thick, tacky, or fiber-reinforced and keeps grabbing the edge instead of shearing cleanly. The right choice depends less on the machine and more on the compound — soft natural rubber, EPDM, silicone, and reinforced conveyor belting all cut differently, and the blade geometry needs to match that behavior.
Why Rubber Behaves Differently Than Plastic or Paper Under a Blade
Here’s the mistake a lot of buyers make: they treat rubber like just another flexible substrate and order whatever blade worked on their last film or paper job. That usually backfires. Rubber has elastic memory — it compresses under the blade edge before it actually shears, which means a dull or wrong-angle blade doesn’t cut, it tears.
That elasticity also generates friction heat fast. On a high-speed slitter, a poorly matched blade can heat up enough to gum the edge with melted rubber residue within minutes. That’s why blade geometry, coating, and edge angle matter more here than on most other materials. If you’re also cutting film or nonwoven substrates on the same line, it’s worth comparing notes with our guide on blades for printing, paper, and nonwoven web handling — the friction dynamics are surprisingly similar.
Straight Blades: The Workhorse for Flat Sheet and Die-Cutting
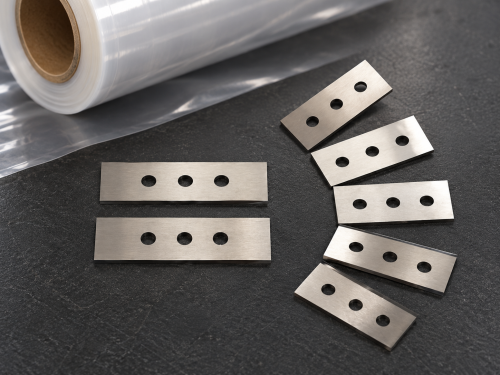
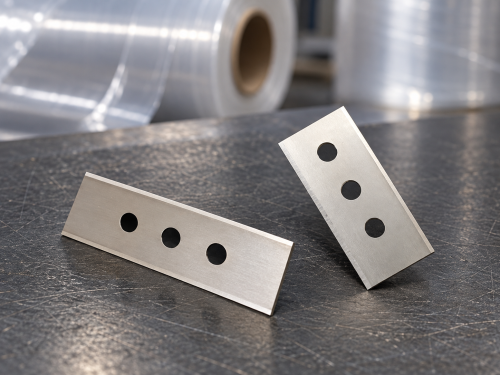
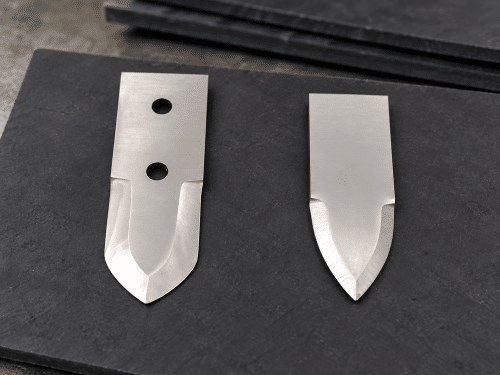
Straight blades are your go-to when you’re cutting flat rubber stock — gasket sheet, mats, or die-cut shapes — and you need a clean, controlled edge every time. They work in guillotine shears, clicker presses, and manual cutting tables.
Where straight blades shine
- Low-to-medium production volumes where precision matters more than speed
- Thin to medium-gauge sheet (under 10mm) with consistent compound density
- Applications requiring a razor-clean edge for sealing or bonding surfaces
The downside? Straight blades struggle on thicker or tackier rubber because the entire edge contacts the material at once — there’s no slicing action to reduce resistance. For gasket manufacturers cutting EPDM sheet, a straight blade with a hollow-ground bevel and a hard chrome or PVD coating usually solves the sticking problem without switching profiles entirely.
Circular Blades: Built for Continuous Roll-to-Roll Slitting
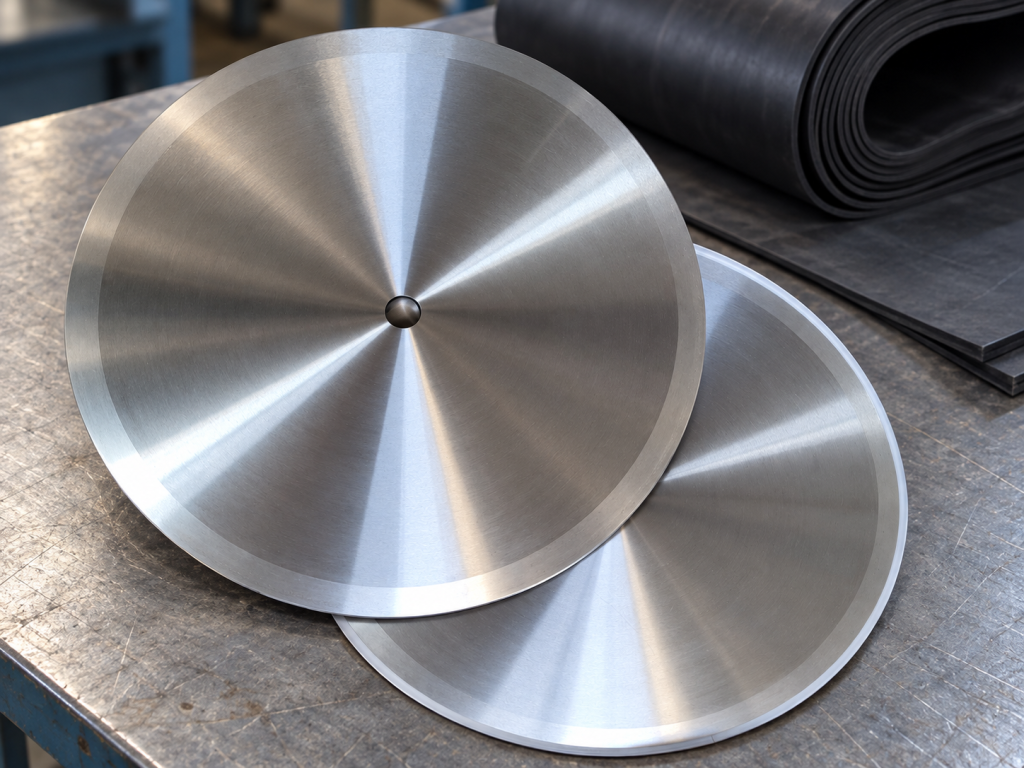
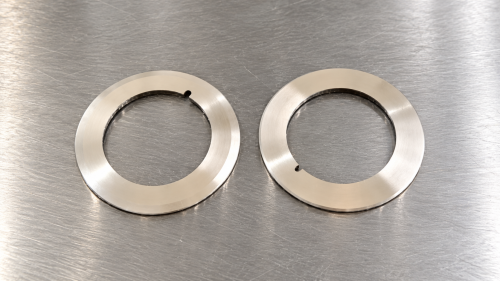
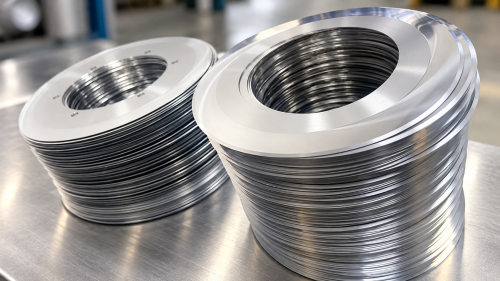
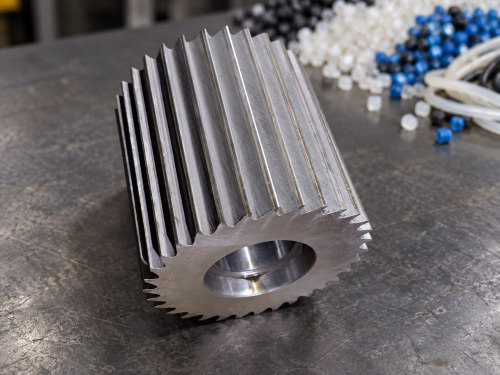
If your line runs rubber off a roll — think extruded rubber strip, calendered sheet, or continuous belting — circular blades are the obvious choice. They rotate continuously with the material feed, which avoids the stop-start shear action that causes tearing on elastic substrates.
For instance, a conveyor belt manufacturer slitting wide rubber sheet into narrower belt widths typically runs paired circular blades in a shear-cut configuration, with tension control keeping the material taut so the blade doesn’t just push the rubber instead of cutting it. Get the tension wrong and you’ll see wavy, uneven edges even with a brand-new blade.
Material and coating matter here
Circular rubber blades usually need a slightly different steel treatment than circular blades used on paper or film — see our breakdown on choosing the right material for circular slitting blades for how substrate changes the alloy and heat treatment decision. On rubber specifically, a non-stick coating (like DLC or Teflon-based) reduces the gumming that kills throughput on long runs.
Serrated Blades: The Answer to Grabby, Reinforced, or Tacky Rubber
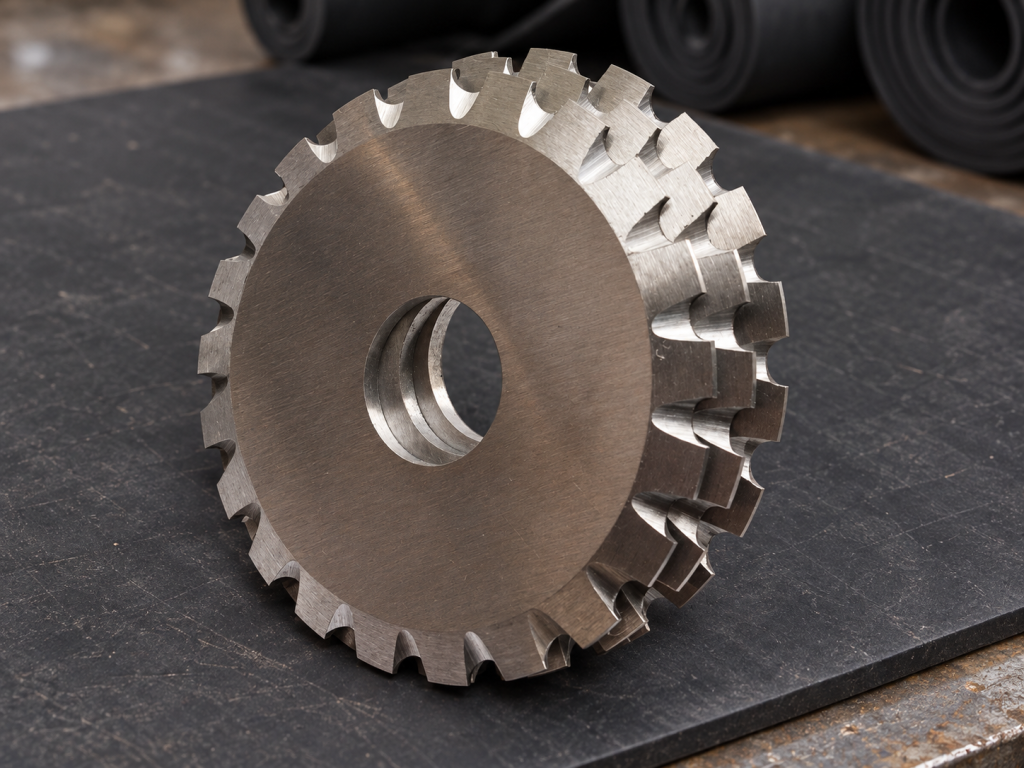
Serrated blades exist because some rubber simply won’t let a smooth edge glide through it cleanly. Fiber-reinforced conveyor belting, high-tack adhesive-backed rubber, and thick silicone gaskets all tend to grip a straight or circular edge and drag rather than shear.
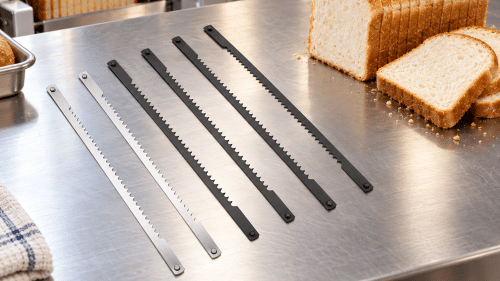
The teeth on a serrated blade reduce the contact surface area at any given moment, which lowers friction and heat buildup dramatically. A recycling equipment OEM we’ve worked with switched from a straight blade to a fine-tooth serrated profile on their rubber crumb pre-shredder specifically because the straight edge was overheating and glazing over within a single shift. The serrated blade ran nearly three times longer between sharpenings.
Serration pitch matters more than people think
- Fine serration (1-2mm pitch): cleaner edge, best for thinner reinforced sheet
- Coarse serration (3-5mm pitch): more aggressive bite, better for thick or heavily fiber-filled rubber
Get the pitch wrong in either direction and you’ll either lose the anti-grab benefit or leave an overly rough edge that needs secondary trimming.
Matching Blade Material to Rubber Compound
Blade profile is only half the equation — the steel or carbide behind that profile decides how long it actually lasts. Natural rubber and softer EPDM compounds are relatively forgiving and run fine on hardened tool steel. Silicone and highly filled compounds (think talc or fiberglass reinforcement) are abrasive and chew through standard steel edges fast.
If you’re processing abrasive or filled rubber compounds at volume, it’s worth reading our comparison on steel vs carbide vs ceramic blade materials before locking in a spec. Carbide-tipped serrated blades, for example, cost more upfront but can outlast standard tool steel by 4-5x on reinforced rubber belting.
Common Mistakes That Shorten Rubber Blade Life
Running the wrong angle for the compound
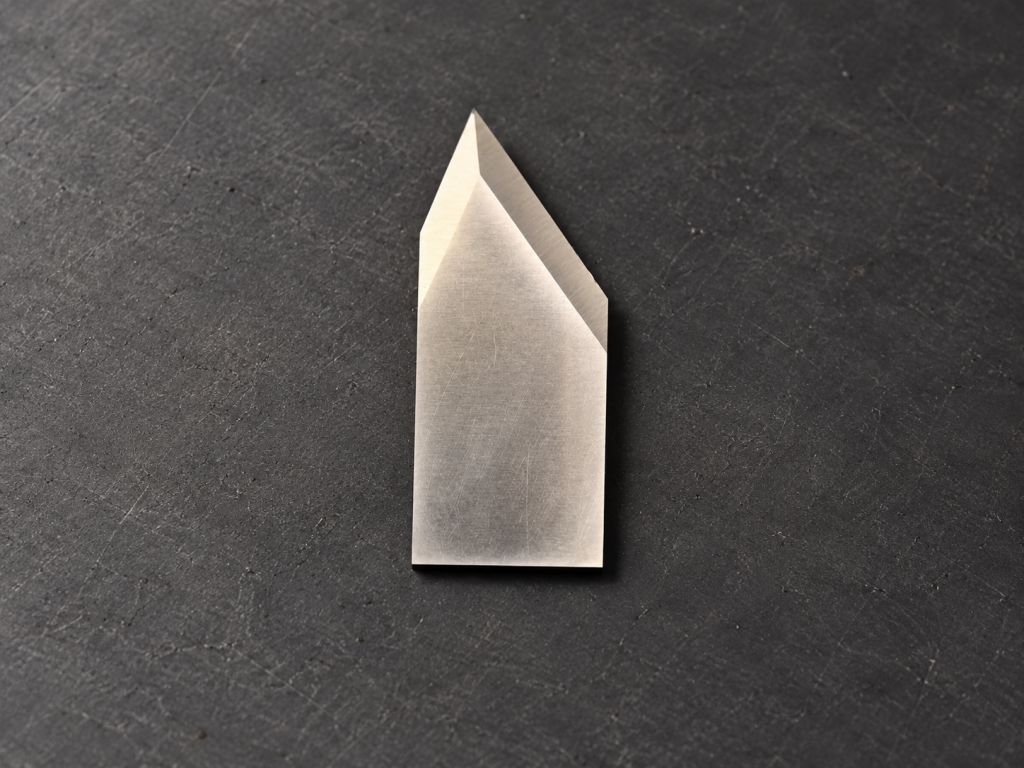
A blade bevel that’s too acute chips easily on hard or filled rubber. Too obtuse, and it pushes rather than shears soft compounds. Most OEM rubber cutting applications land somewhere between 20-30 degrees, but that’s a starting point, not a rule.
Ignoring heat buildup
Rubber’s elasticity generates friction heat that steel doesn’t dissipate well without coating or airflow assistance. If you’re seeing a burnt rubber smell during cutting, that’s your early warning sign — not something to run through until the blade fails.
Skipping trial runs on new compounds
Switching rubber suppliers or compounds without validating blade performance is a common and costly mistake. A quick trial order run — even a short batch — catches mismatches before they show up as scrapped production runs. This is standard practice we recommend to OEMs before committing to volume orders.
Extending Blade Life Once You’ve Picked the Right Profile
Even the perfect blade profile degrades faster than it should if sharpening intervals and storage aren’t managed properly. Rubber residue buildup, moisture exposure, and improper stacking all accelerate wear regardless of whether you’re running straight, circular, or serrated edges.
Our guide on extending industrial blade service life covers sharpening intervals and wear pattern diagnosis in more detail, but for rubber specifically, cleaning the edge between shifts to remove sticky residue buildup is the single easiest way to add weeks to blade life.