
Pneumatic Slitting Knives: How They Work and Where They Are Used
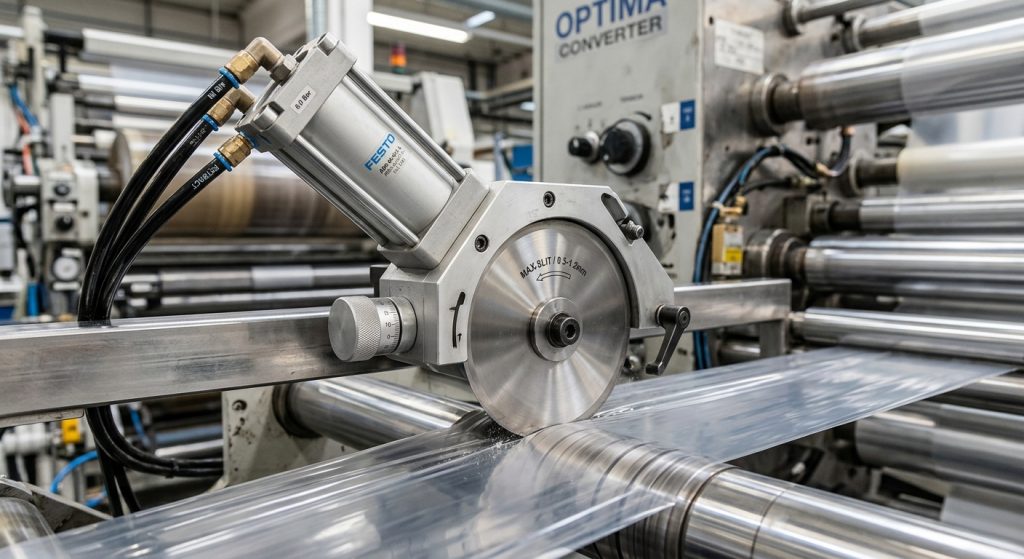
Pneumatic slitting knives cut using compressed air to push the blade holder against the anvil or mating knife, instead of relying on fixed springs or manual screw tension. That air-driven pressure can be adjusted in real time — even while the line is running — which is exactly why pneumatic systems have become the go-to choice for film, foil, and nonwoven converting lines that need to switch materials fast. The core advantage isn't cutting power; it's control.
The Mechanism: What Actually Happens Inside a Pneumatic Slitter Head
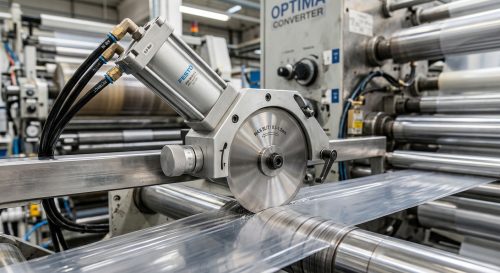
Here's the part most people get wrong: pneumatic slitting isn't about air blasting the blade forward at high speed. It's about a controlled, low-force actuator holding steady contact pressure between a rotating top knife and a bottom anvil or shear knife.
A small pneumatic cylinder — usually rated between 0.5 and 6 bar depending on the machine — pushes a mounting arm that carries the circular blade. Increase the air pressure, and contact force at the cutting edge increases proportionally. Drop it, and the blade lifts or reduces pressure almost instantly. This is why operators can dial in cutting force to match a 12-micron BOPP film one minute and a 40-gsm nonwoven the next, without swapping hardware.
Why This Beats a Fixed Spring
Springs give you one pressure curve. Once compressed to spec, that's it until someone manually re-tensions it — usually with the line stopped. Pneumatic systems let you nudge pressure up or down from a control panel, sometimes even per-knife-station if the machine has individually zoned air lines.
Score Cutting vs. Shear Cutting: Two Very Different Pneumatic Setups
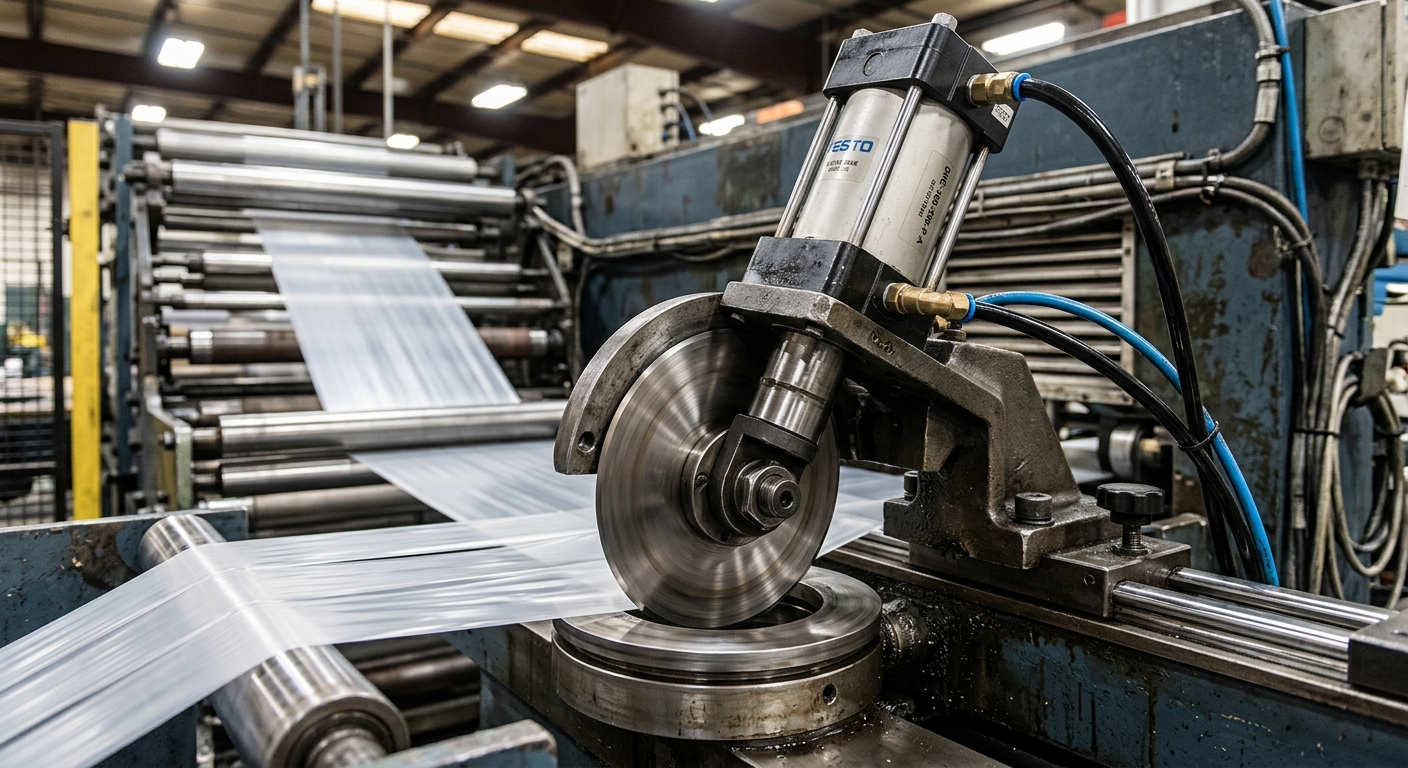
Not all pneumatic slitting is the same operation. Score (razor) slitting and shear slitting use pneumatic pressure completely differently, and mixing them up leads to bad cuts.
In score slitting, a razor blade presses through the film against a hardened steel anvil roller. Air pressure here just needs to be enough to fully penetrate the material — usually a light, consistent touch. Too much pressure and you're grinding the razor edge into the anvil, cutting blade life dramatically.
In shear slitting, a male-female circular blade pair overlaps slightly and shears the material like scissors. Pneumatic pressure controls the overlap engagement force, not penetration depth. This method handles heavier, tougher substrates — think laminated films, coated papers, thin metal foils — that a razor would just push around instead of cutting cleanly.
For a deeper look at how blade geometry and material choice change these outcomes, see our guide on choosing the right material for circular slitting blades.
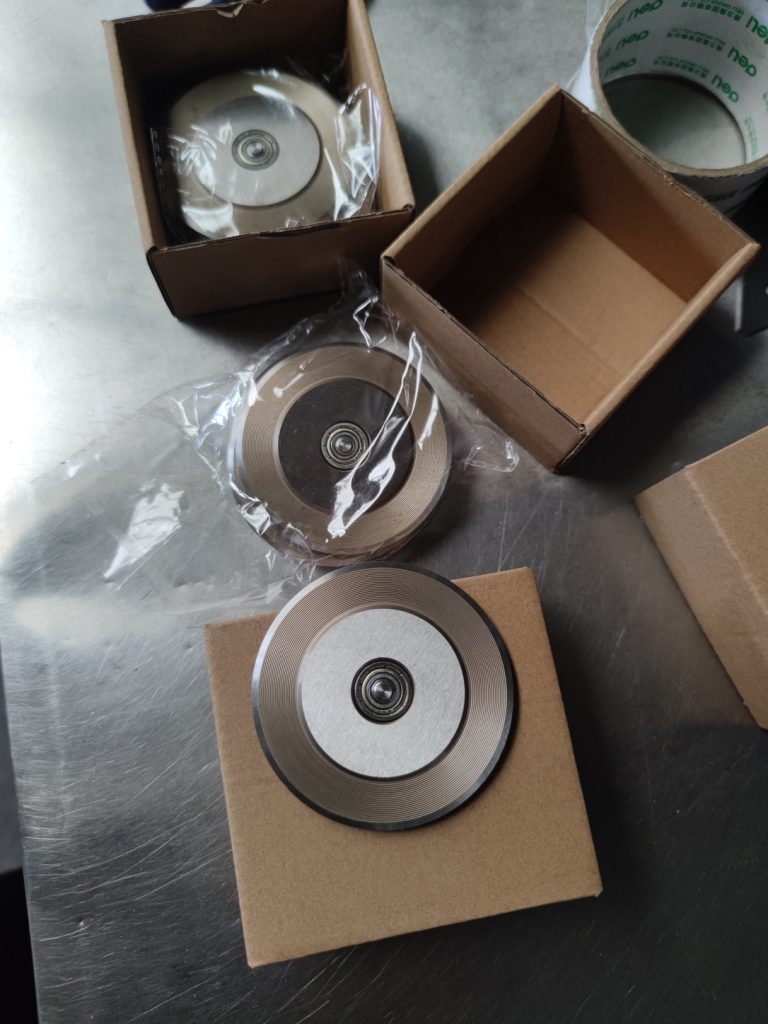
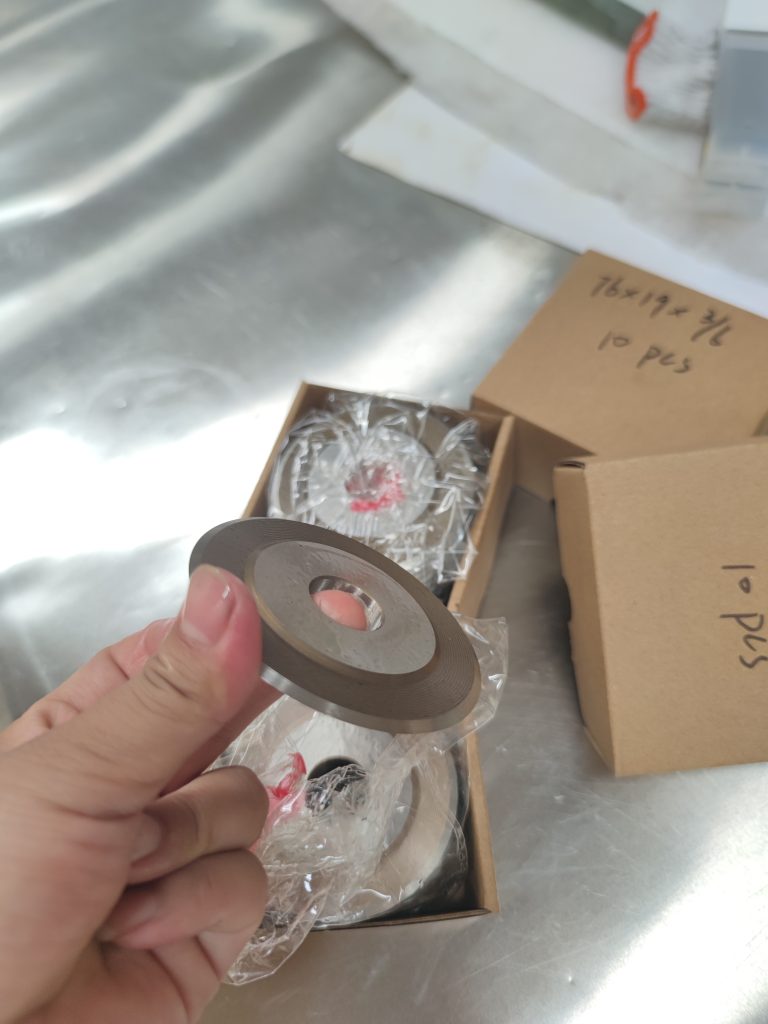
Where Pneumatic Slitting Knives Actually Get Used
You'll find pneumatic slitting almost anywhere thin, flexible material moves fast through a web line. It's less common on heavy metal coil lines, where hydraulic or mechanical shear systems dominate.
Flexible Packaging and Film Converting
BOPP, PET, and PE film lines running at 300-500 m/min rely on pneumatic score slitters because pressure needs constant fine-tuning as roll diameter, tension, and film gauge shift during a run. A converter switching between a 20-micron retort pouch film and a thicker 60-micron stand-up pouch laminate can rezero pressure in seconds rather than stopping the line to swap spring tension.
Nonwoven and Hygiene Product Lines
Diaper, wipes, and medical nonwoven producers use pneumatic slitting to trim edges and slit multi-lane webs without crushing the fibrous structure. Too much mechanical force here causes fraying; pneumatic control keeps pressure just above the cutting threshold.
Paper and Label Slitting
Label stock and coated paper slitting benefit from pneumatic pressure because coating weight varies batch to batch. Related equipment and blade options are covered on our paper and web handling blades page.
For packaging-specific blade geometry questions, our packaging blade types guide breaks down cutting method selection in more depth.
A Real Case: Switching a Laminate Line from Spring to Pneumatic
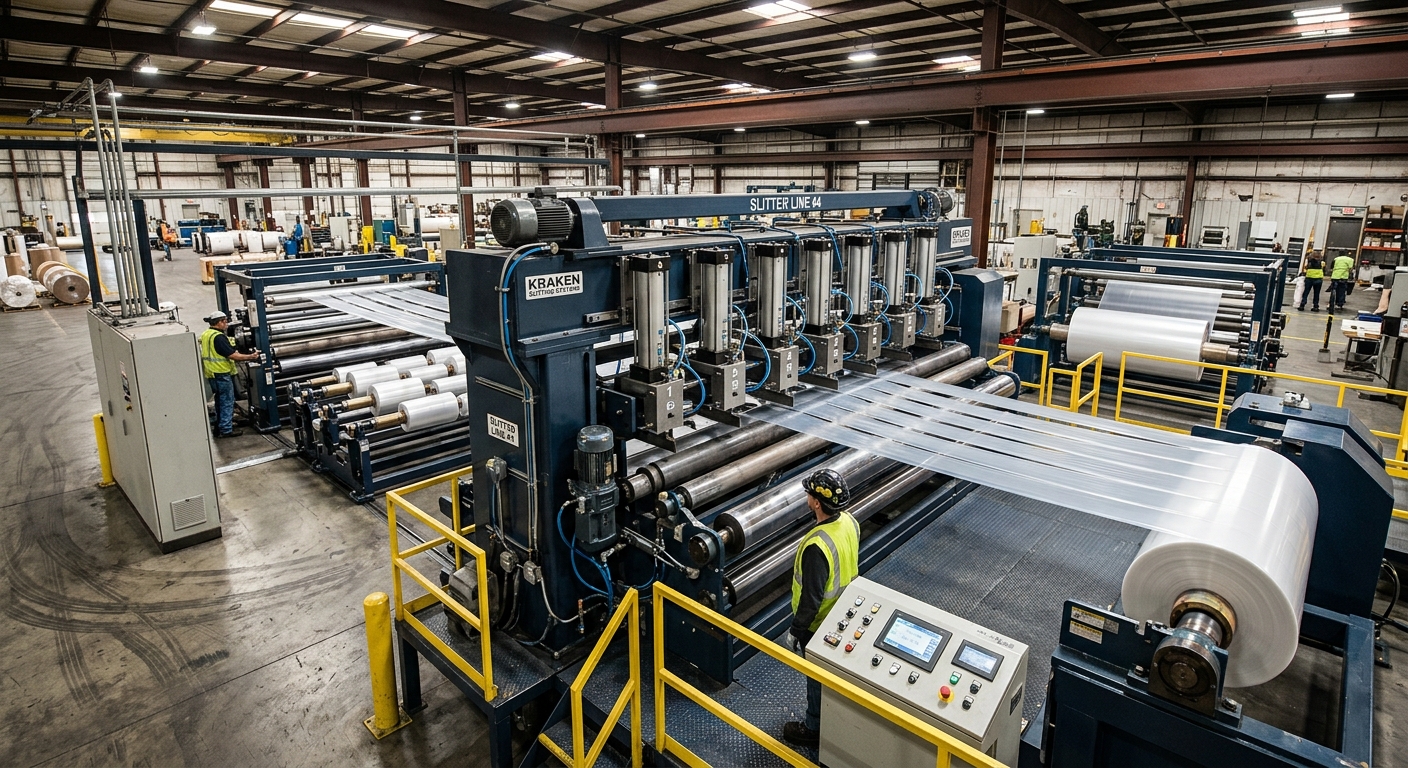
A mid-size flexible packaging plant we worked with was running spring-loaded score slitters on a laminate line producing both snack film and pet food pouch stock. Every product changeover meant stopping the line for 15-20 minutes to manually re-tension six slitting stations.
After switching to a pneumatic slitting head setup with a shared air manifold, changeover pressure adjustment dropped to under 90 seconds — done from the operator panel without touching the blades. Blade life also improved by roughly 18% because operators stopped over-tightening springs “just to be safe,” which had been accelerating edge wear. The lesson: pneumatic control doesn't just save changeover time, it protects the blade itself from human overcorrection.
Blade Material Still Matters — Air Pressure Can't Fix a Bad Blade
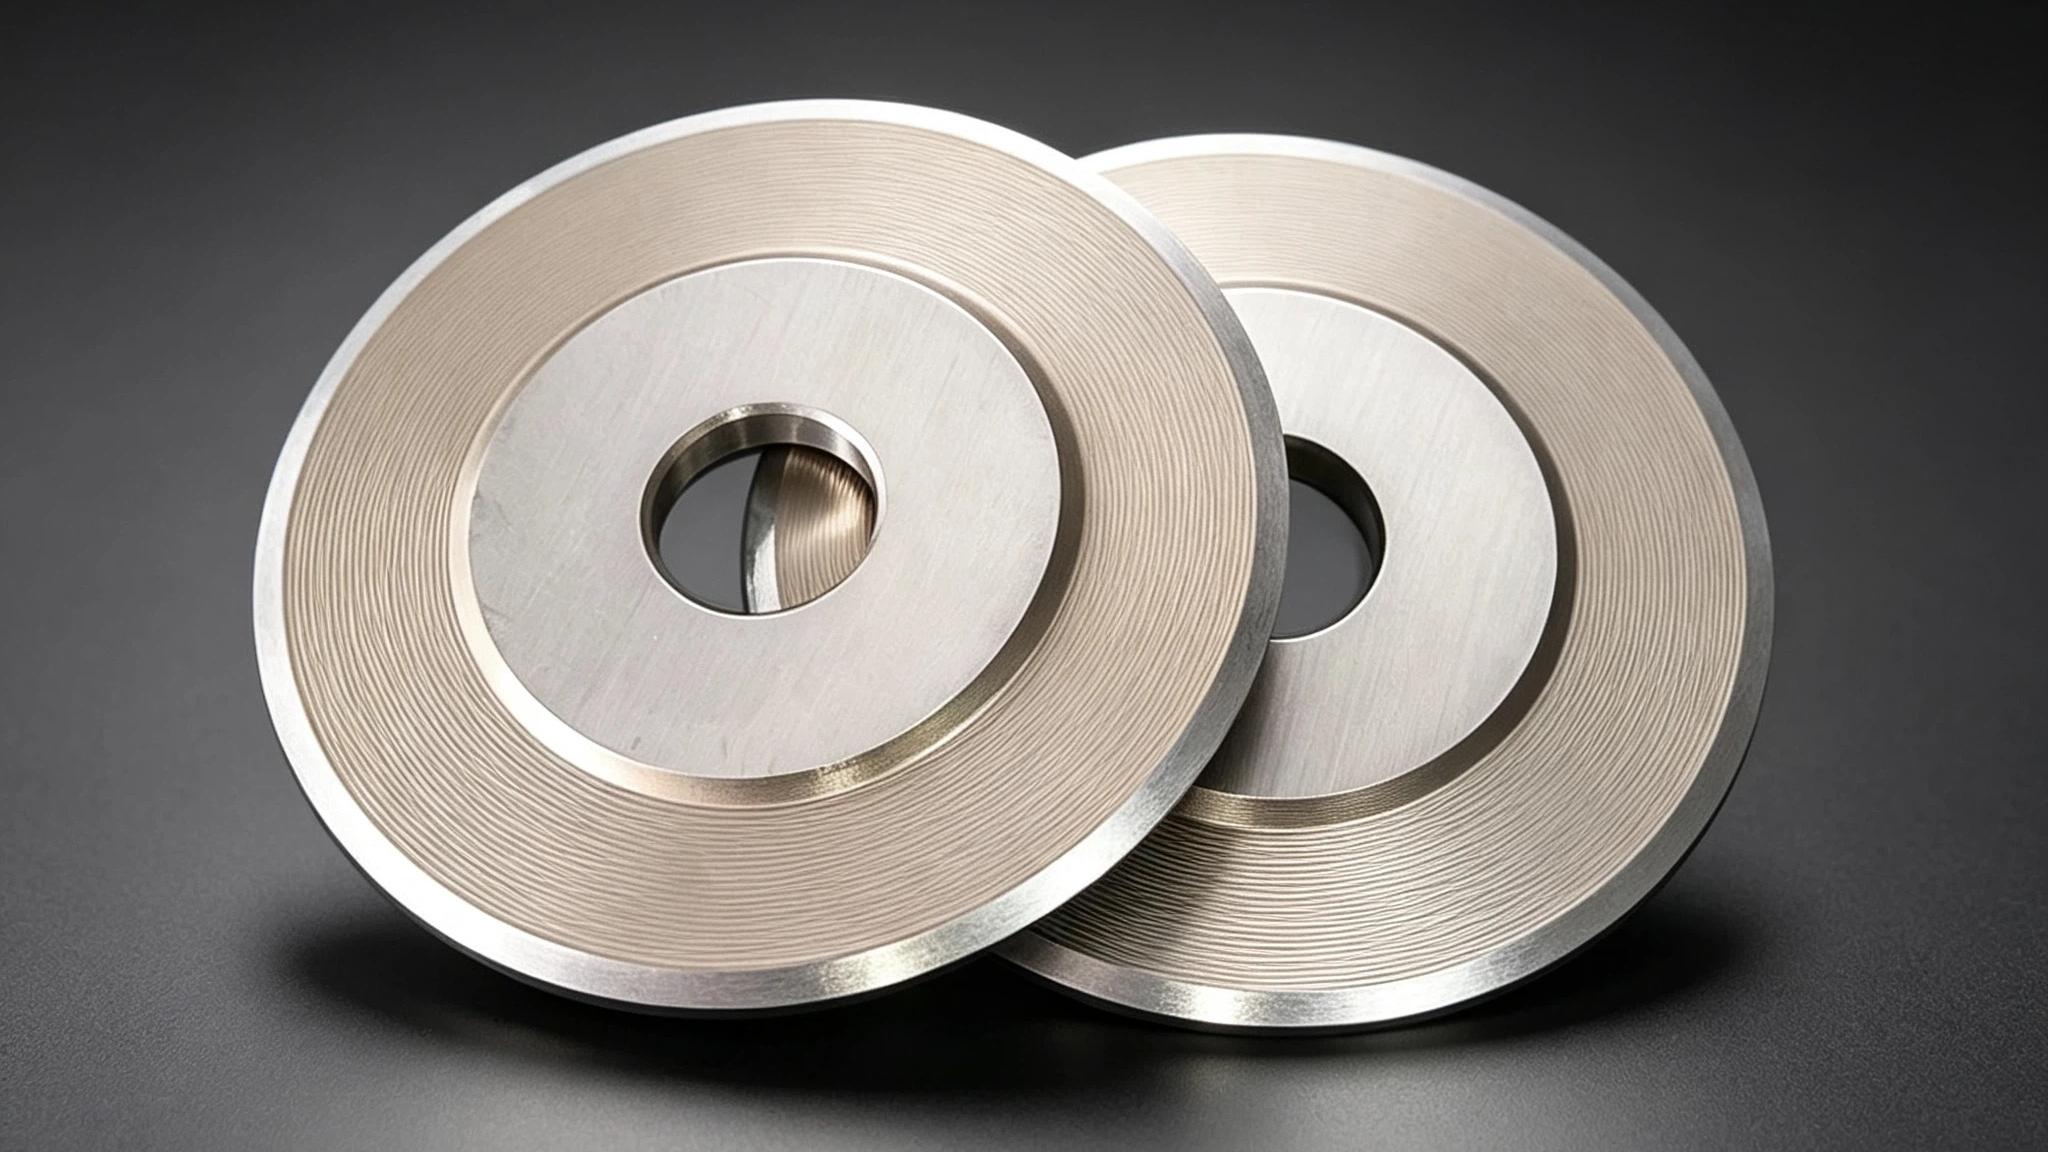
Pneumatic systems control force, not edge geometry or hardness. If the blade material is wrong for the substrate, no amount of pressure tuning saves the cut quality.
Tungsten carbide blades hold an edge far longer on abrasive coated films and fiber-loaded nonwovens, while high-speed steel works fine on cleaner, less abrasive films at a lower cost per blade. Choosing wrong here means you'll be compensating with higher pneumatic pressure just to force a dulling edge through material — which burns through blades even faster. Our comparison on steel vs. carbide vs. ceramic blade material walks through how to match material to substrate abrasiveness and run volume.
Common Problems Pneumatic Systems Introduce (and How to Avoid Them)
Pneumatic slitting isn't maintenance-free. The air system itself becomes a new point of failure if it's neglected.
- Moisture in the air line causes inconsistent pressure delivery — install a proper filter/regulator/lubricator (FRL) unit and check it monthly.
- Pressure drift over a shift happens when compressor output fluctuates under plant-wide demand. Dedicated regulators at each slitting station prevent this.
- Operators setting pressure by feel instead of by spec sheet, leading to inconsistent cuts between shifts. Document target PSI per material grade and post it at the station.
If you're already seeing inconsistent edge quality, it's worth ruling out these pneumatic-specific issues before blaming the blade. Our post on why slitting lines produce burrs covers the broader troubleshooting checklist, including blade-related causes that look similar to pressure problems.
Specifying a Pneumatic Slitting Knife: What to Tell Your Blade Supplier
Getting the right blade for a pneumatic setup means giving your supplier more than just a diameter and bore size. At minimum, share:
- Substrate type, thickness, and abrasiveness (coated, filled, laminated, etc.)
- Target line speed and expected run length between changeovers
- Whether it's score or shear slitting
- Current pneumatic pressure range on your machine
- Whether you need OEM-matched geometry or are open to a redesigned profile for longer wear life
This is essentially the same information needed for any custom industrial blade order — the pneumatic detail just helps the engineer estimate real-world contact force and recommend a matching hardness and edge angle.